How Roll-On Bottles Are Manufactured for Consistent Bulk Production
A roll-on bottle has fewer moving parts than a spray pump, but that does not make the package technically simple.
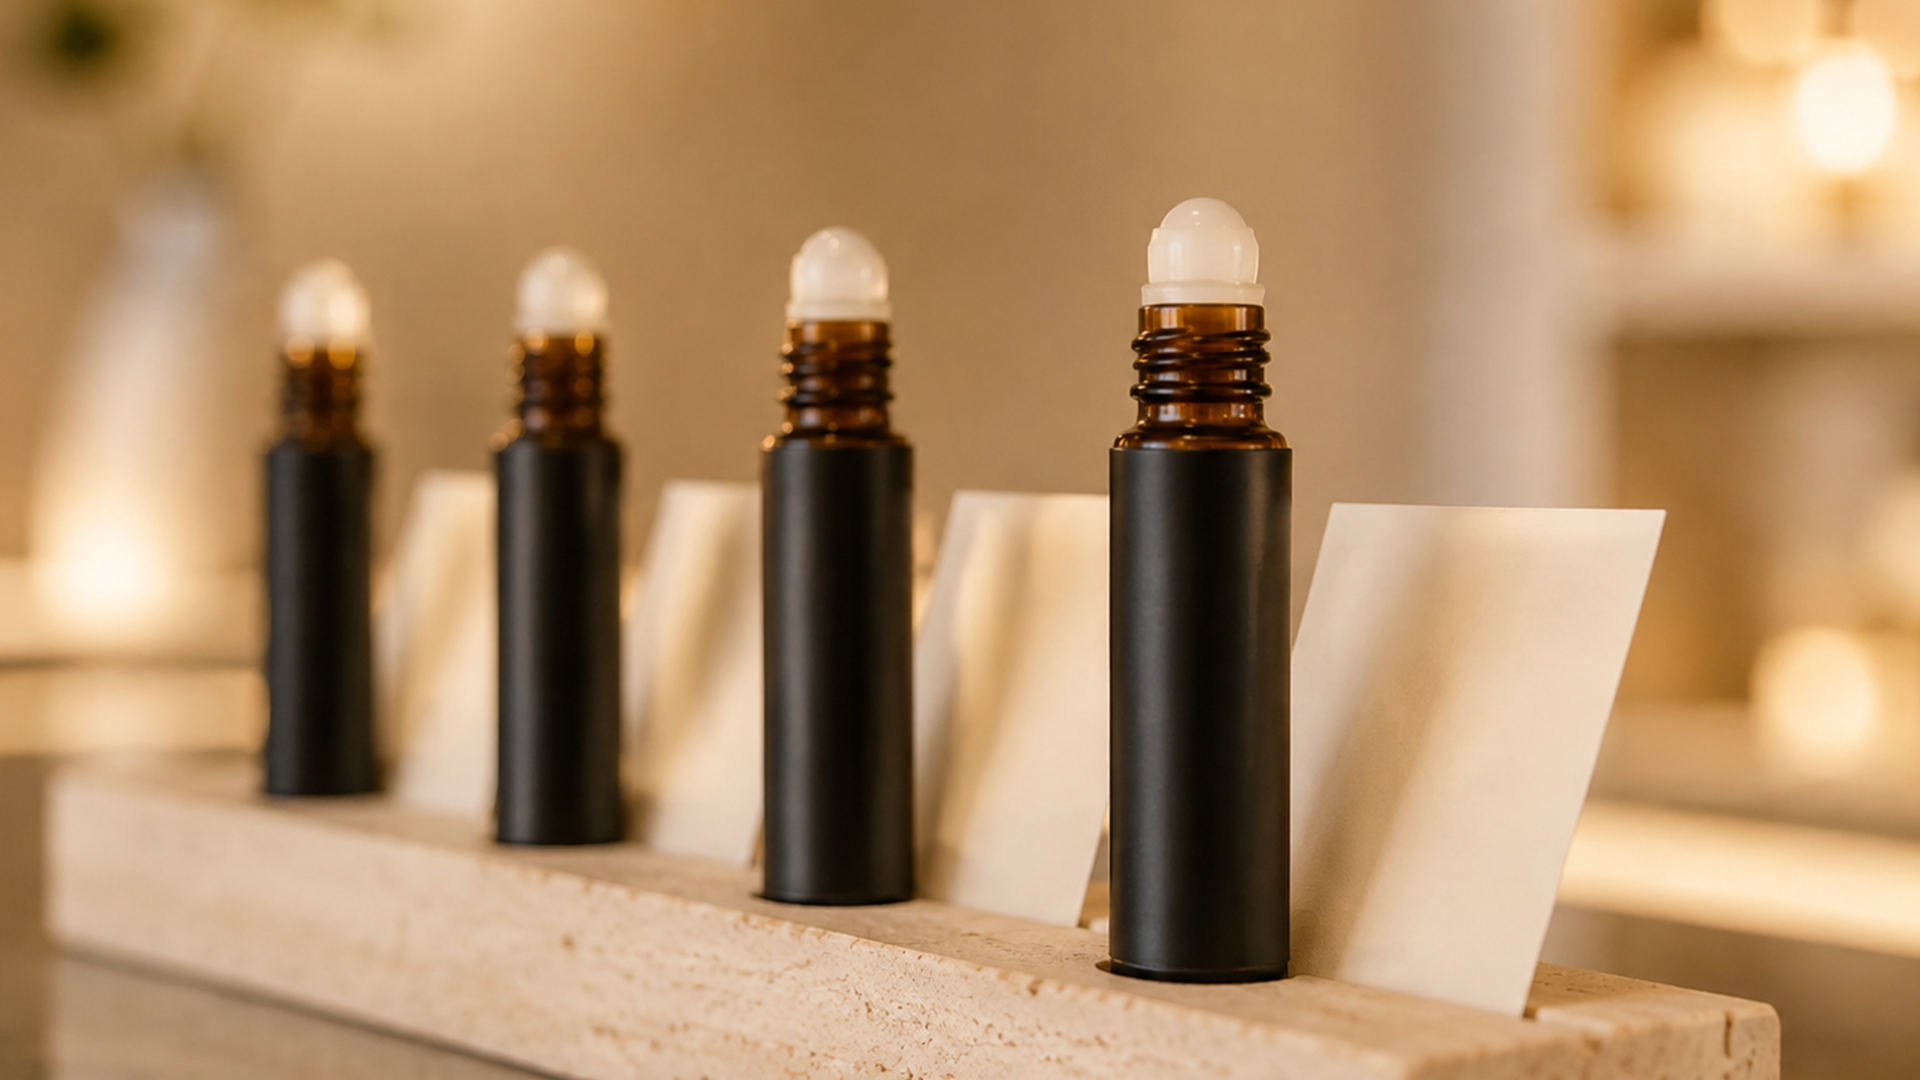
The most critical area is the connection between three components:
bottle neck + ball housing + roller ball
The clearances between these parts determine whether the ball rotates smoothly, dispenses enough product and remains sealed during transportation.
For large-volume buyers, this dimensional relationship is one of the most important quality-control points.
The Roller Ball Is a Precision Component
Roller balls may be produced from materials such as:
- PP
- PE
- stainless steel
- glass
- other application-specific materials
The correct material depends on formulation, cost, product positioning and required dispensing feel.
Regardless of material, ball diameter needs to be tightly controlled.
If the ball is too large relative to the housing, rotation becomes difficult.
If it is too small, excessive liquid release or leakage can occur.
Ball Roundness Matters
A roller ball should not only meet nominal diameter.
Roundness and surface quality affect rotation.
Visible molding marks, deformation or surface defects can create:
- uneven rolling
- scratching sensation
- inconsistent application
- local leakage
For premium cosmetic roll-on products, the tactile quality of the ball is part of the user experience.
Ball Housing Manufacturing
The ball housing—or fitment—is usually a molded component inserted into the bottle neck.
Its internal geometry controls:
- ball retention
- rolling resistance
- product transfer
- sealing behavior
The housing must hold the ball securely while still allowing free rotation.
That balance requires relatively precise molding.
Bottle Neck Tolerance
Roll-on packages are particularly sensitive to bottle neck variation.
If the neck is too large, the insert may not lock securely.
If too small, insertion force may become excessive or the neck may deform.
For this reason, bulk buyers should approve the bottle and roll-on fitment as one system.
Changing one component supplier during production may require re-testing.
Press-Fit Assembly
Many roll-on systems use a press-fit insert.
The assembly process needs to control insertion depth and force.
For automated production, fixtures can help ensure that each fitment is installed to the same position.
An incorrectly seated fitment can lead to:
- leakage
- loose assembly
- poor cap fit
- inconsistent ball movement
Typical Roll-On Sizes
Depending on application, roller balls may be offered in many diameters, including smaller cosmetic sizes and larger deodorant formats.
Typical market options can include approximately:
15 mm
18 mm
20 mm
25 mm
30 mm
and larger formats.
Exact dimensions depend on the bottle and housing design.
Formula Viscosity and Roll-On Performance
A low-viscosity liquid flows around the ball more easily than a thick gel.
The spacing around the ball therefore needs to match the intended formulation.
When testing a roll-on package, evaluate:
- startup flow
- product transfer
- rolling smoothness
- leakage
- flow after storage
- performance at different temperatures
A roll-on package that works with water may behave very differently with deodorant, essential oil or cosmetic serum.